Performance Exhaust Systems
Performance Exhaust System Manufacturer
The production side of the range: what is made, how it is made, and how it is checked, stated plainly.
Torvane is the manufacturer behind the range: the manifolds, downpipes, catback systems, charge pipes and intake manifolds are designed, bent, welded and checked in one workshop, and sold factory-direct. The production side is described in the terms a buyer auditing a supplier actually needs — the processes run, the order they run in, and the checks a part passes before it is packed.
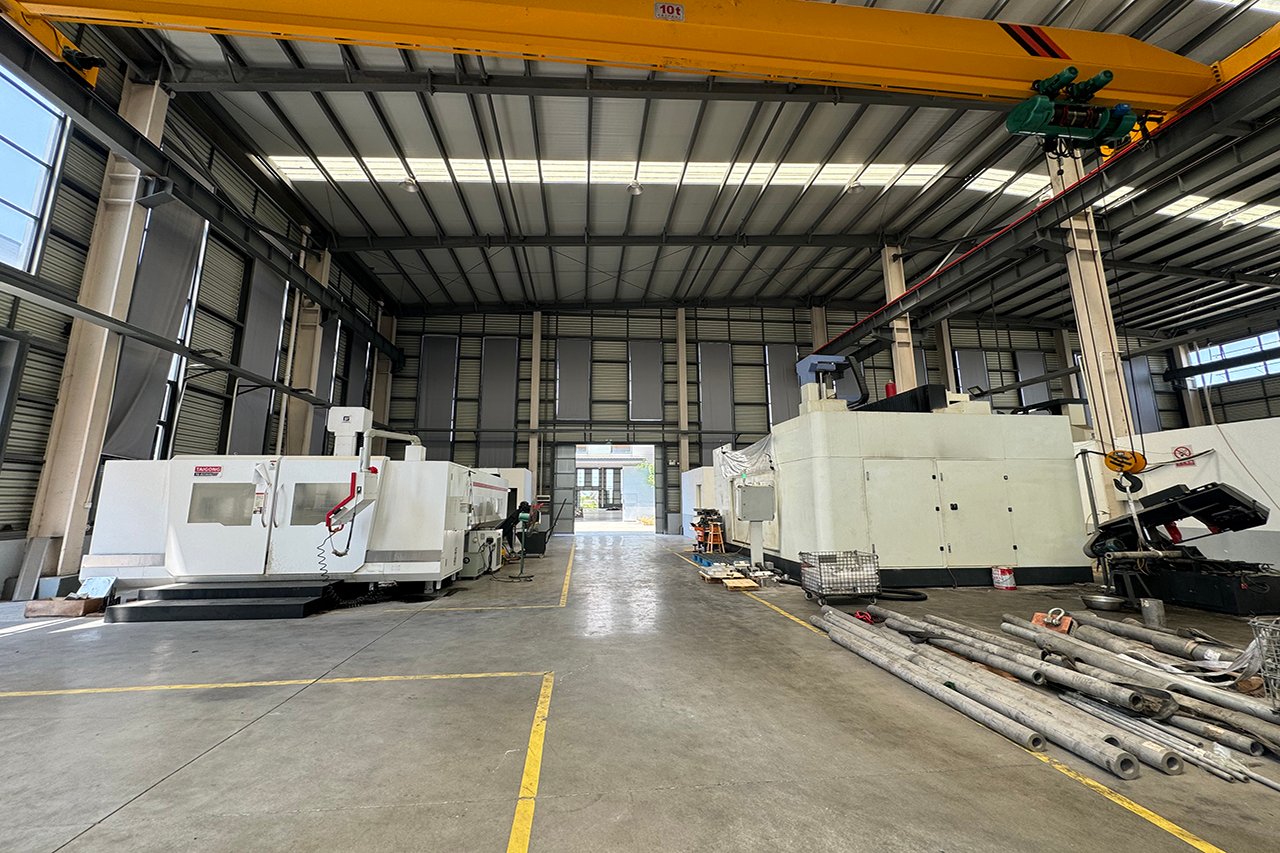
- In-house machiningFlanges and fixtures
- CNC bendingMandrel pipe bending
- TIG weldingOn production fixtures
- Four named checksDimension, weld, leak, fitment
Design and Fixtures
Design starts from the original part: 3D scanning of the OEM piece or the chassis, CAD design from that data, and fixtures built before production — laser-cut and CNC-machined jigs that hold each part in its installed geometry. Flanges are machined on multi-axis CNC centres to the port profile of the engine they serve. The fixture is the manufacturer's memory: it is what makes the hundredth part a copy of the approved first one.
Cutting, Bending and Welding
Pipe is laser cut and bent on CNC mandrel benders. Welding is TIG — argon-shielded for titanium work — carried out on the fixtures, with automatic welding where the joint suits it. Collectors are cast, wire-cut or printed, per the design. Finishing is in-house: brushed, mirror polished, burnt blue, vacuum ion plating and ceramic coating.
| Stage | Process | Purpose |
|---|---|---|
| Design | 3D scan, CAD, fixture build | Fitment captured before metal is cut |
| Forming | Laser cutting, CNC mandrel bending | Repeatable tube geometry |
| Joining | TIG welding on fixtures | Joints made in installed geometry |
| Finishing | Brush, polish, burnt blue, plating, ceramic | Specified finish applied in-house |
| Checking | Dimensional, weld, smoke/leak, in-car | Nothing packs unchecked |
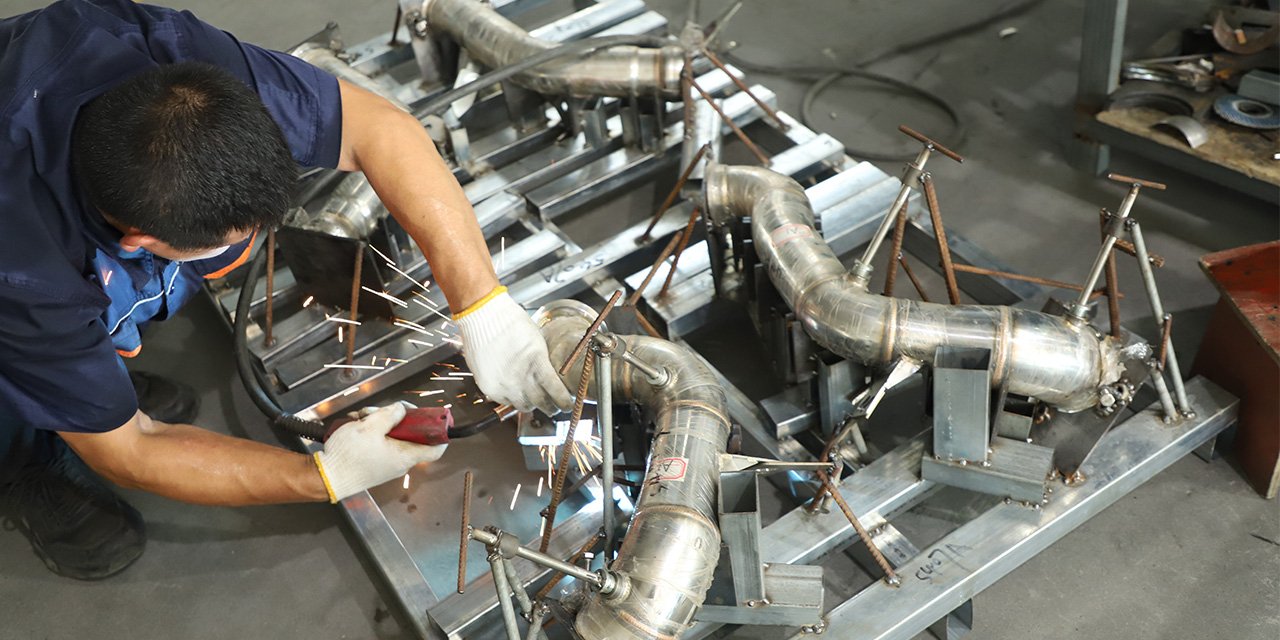
Quality Checks Before Packing
The checks are named because they are specific: dimensional inspection against the fixture; weld testing for airtightness and strength; a smoke and leak test on the assembled part; and in-car fitment checks during development, so production parts inherit a proven fit. Visual and packaging inspection close the sequence. A part that fails a check returns to the bench, not to the crate.
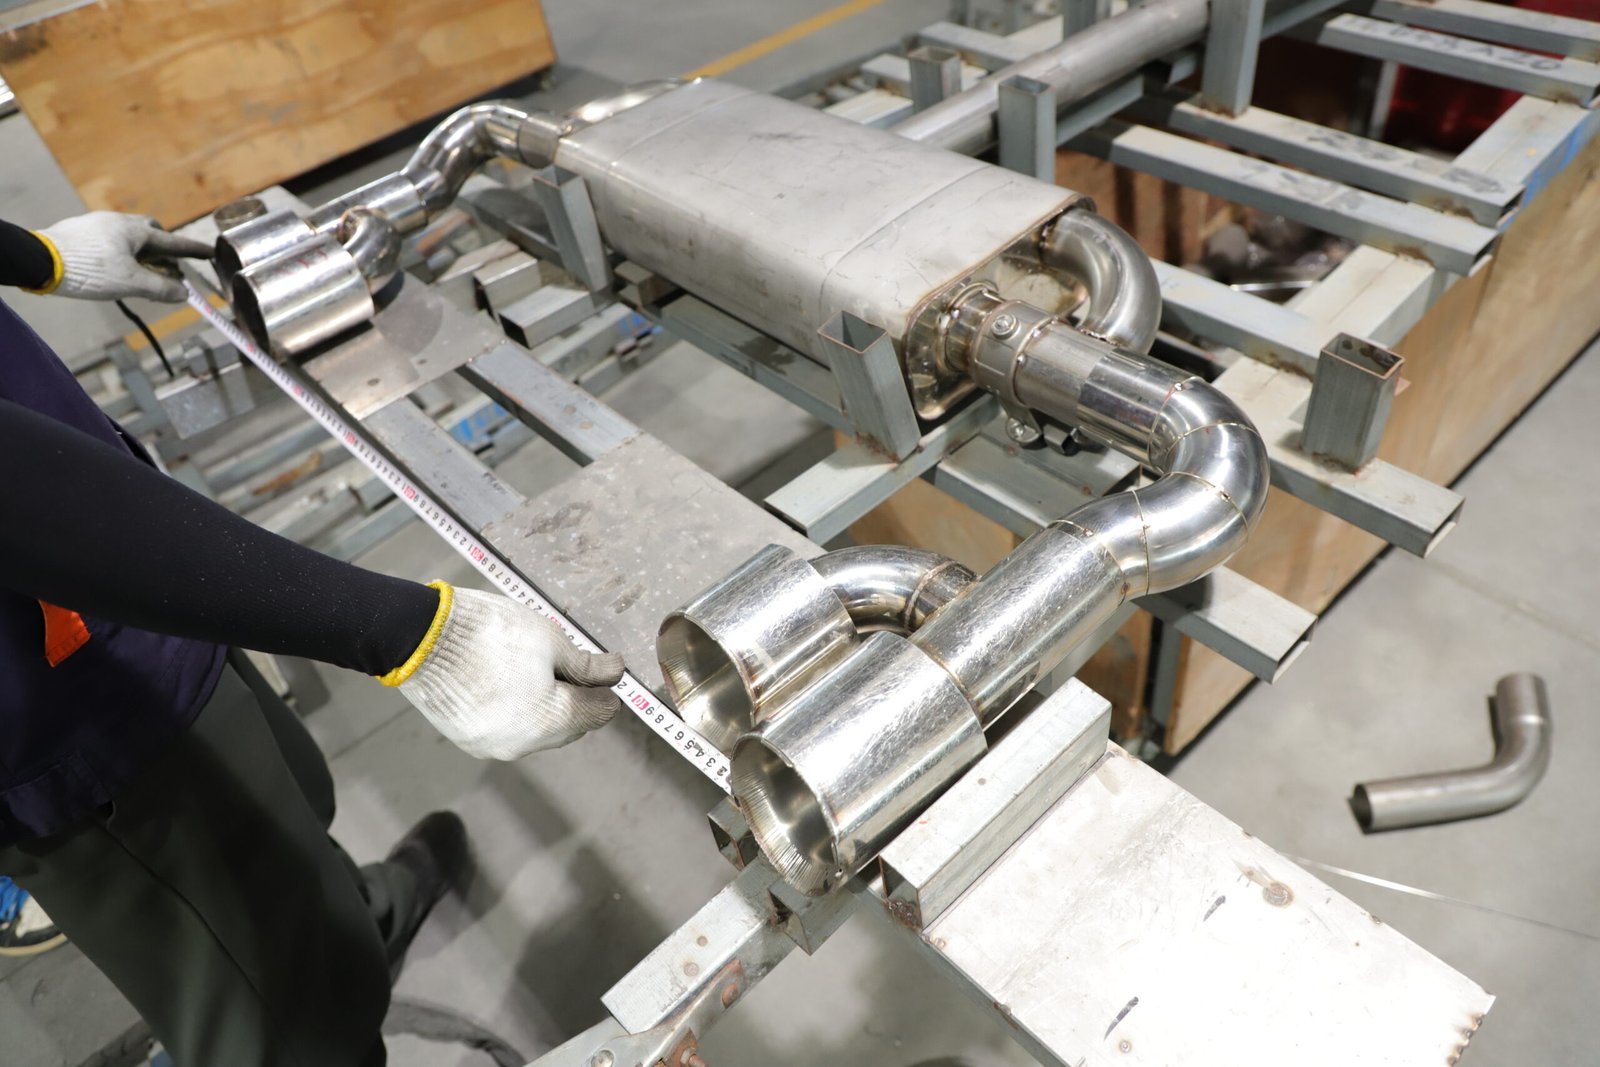
What Factory-Direct Means for a Buyer
It means the quotation, the development conversation and the production schedule sit in the same building as the benches. When a wholesaler asks whether a variant exists for an engine, the answer comes from the fixture record. When a brand asks for its logo etched and its own tip design, the work is specified into the production route rather than subcontracted after it. That is the whole content of the claim, and it is verifiable at sample stage: order one part and inspect what the process produces.
Send Your Vehicle, Engine and Item List
One form covers the whole range. Your list is checked against current production before a quotation comes back.
Send an Inquiry